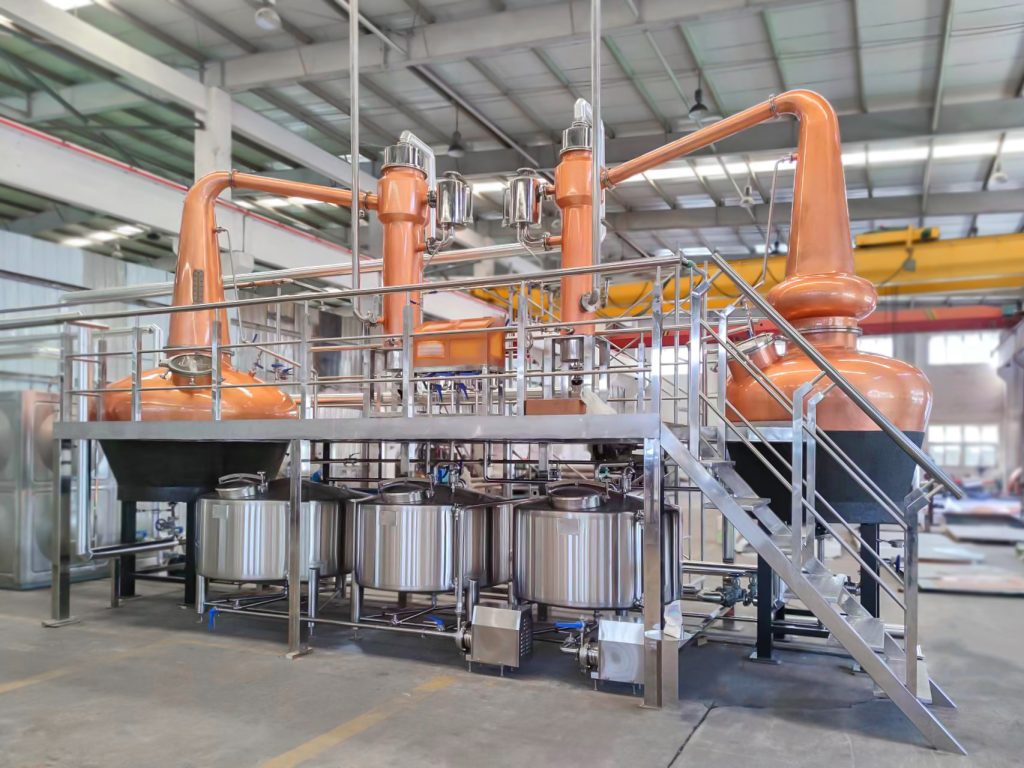
For production breweries that want to start making spirits, choosing the right industrial distillation equipment is very important. Good equipment helps you make consistent, high-quality spirits. It also affects your production capacity and energy costs.
At SKE, we provide customized distillation solutions for commercial and large-scale production. Our experience in brewing and beverage equipment helps us offer complete systems that work well with your existing operations.
This guide explains what to look for in industrial distillation equipment and why SKE is a good partner for your project.
What Is Industrial Distillation Equipment?
Industrial distillation equipment is used to separate alcohol from fermented liquid. The process uses heat and condensation. Alcohol boils at a lower temperature than water. When you heat the liquid, the alcohol turns into vapor first. Then the vapor is cooled and becomes liquid again .
For large-scale spirits production, a complete distillation system includes several parts:
-
Pot stills or column stills
-
Dephlegmators for reflux control
-
Condensers for cooling vapor
-
Steam heating systems
-
Spirit collection systems
-
Pumps and valves
-
Temperature and pressure sensors
-
Control systems
The right system depends on what spirit you want to make and how much you want to produce. SKE designs equipment based on your specific needs.
Why Equipment Quality Matters for Production Breweries
A production brewery faces different challenges than a small craft distiller. When you produce more, small problems become big problems.
Uneven heating can ruin a batch. Poor vapor control reduces how well you separate alcohol. Inconsistent temperature makes it hard to repeat good results.
High-quality industrial distillation equipment solves these problems. It gives you controlled heating, stable vapor flow, efficient condensation, and accurate monitoring.
Material choice is also important. Food-grade stainless steel is the industry standard. It is strong, durable, hygienic, and easy to clean. Many systems also use copper because copper helps remove sulfur compounds that cause bad flavors.
SKE uses high-grade stainless steel (304/316L) and adds copper where it helps spirit quality. Our equipment meets international standards like PED and ASME. This ensures safety and compliance for global markets.
Pot Still vs. Column Still: Which One Do You Need?
When you choose industrial distillation equipment, one key decision is whether to use a pot still or a column still. Both have different uses.
Stainless Steel Pot Still
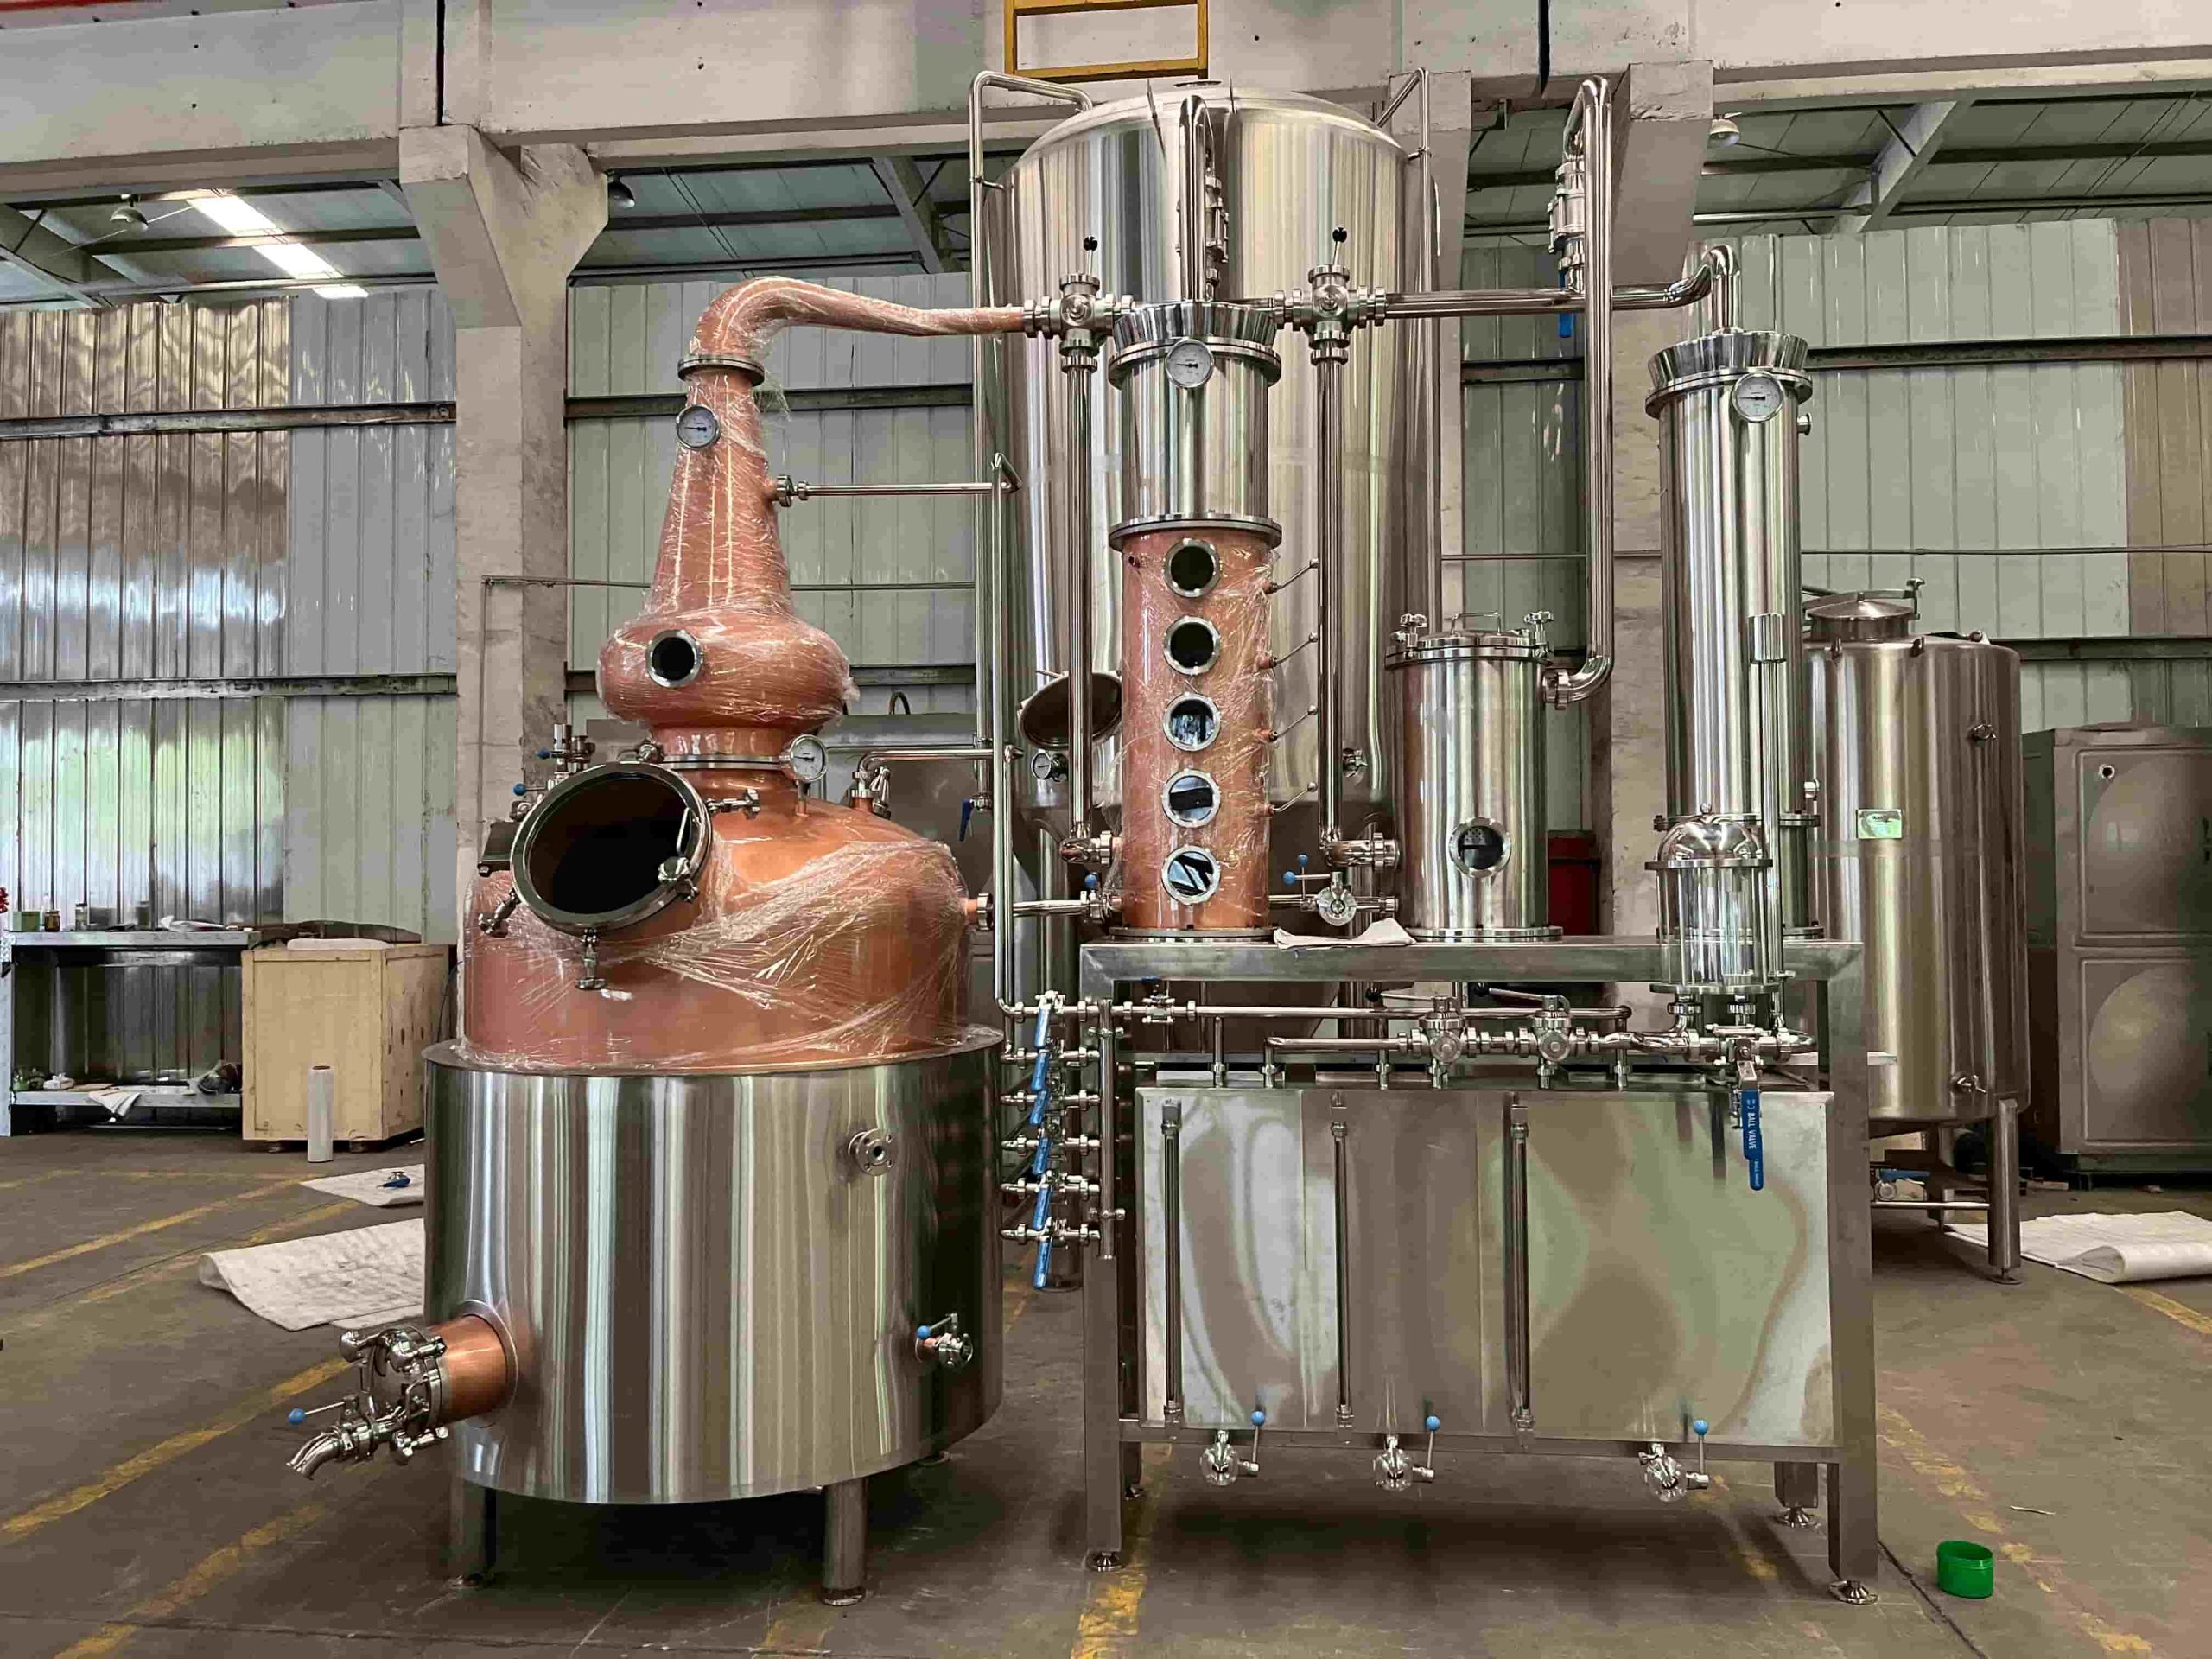
A stainless steel pot still is commonly used for whiskey, rum, and brandy. These are spirits where flavor and character are very important. The fermented wash is heated in batches. The still’s shape, heating method, vapor path, and condenser all affect the final spirit.
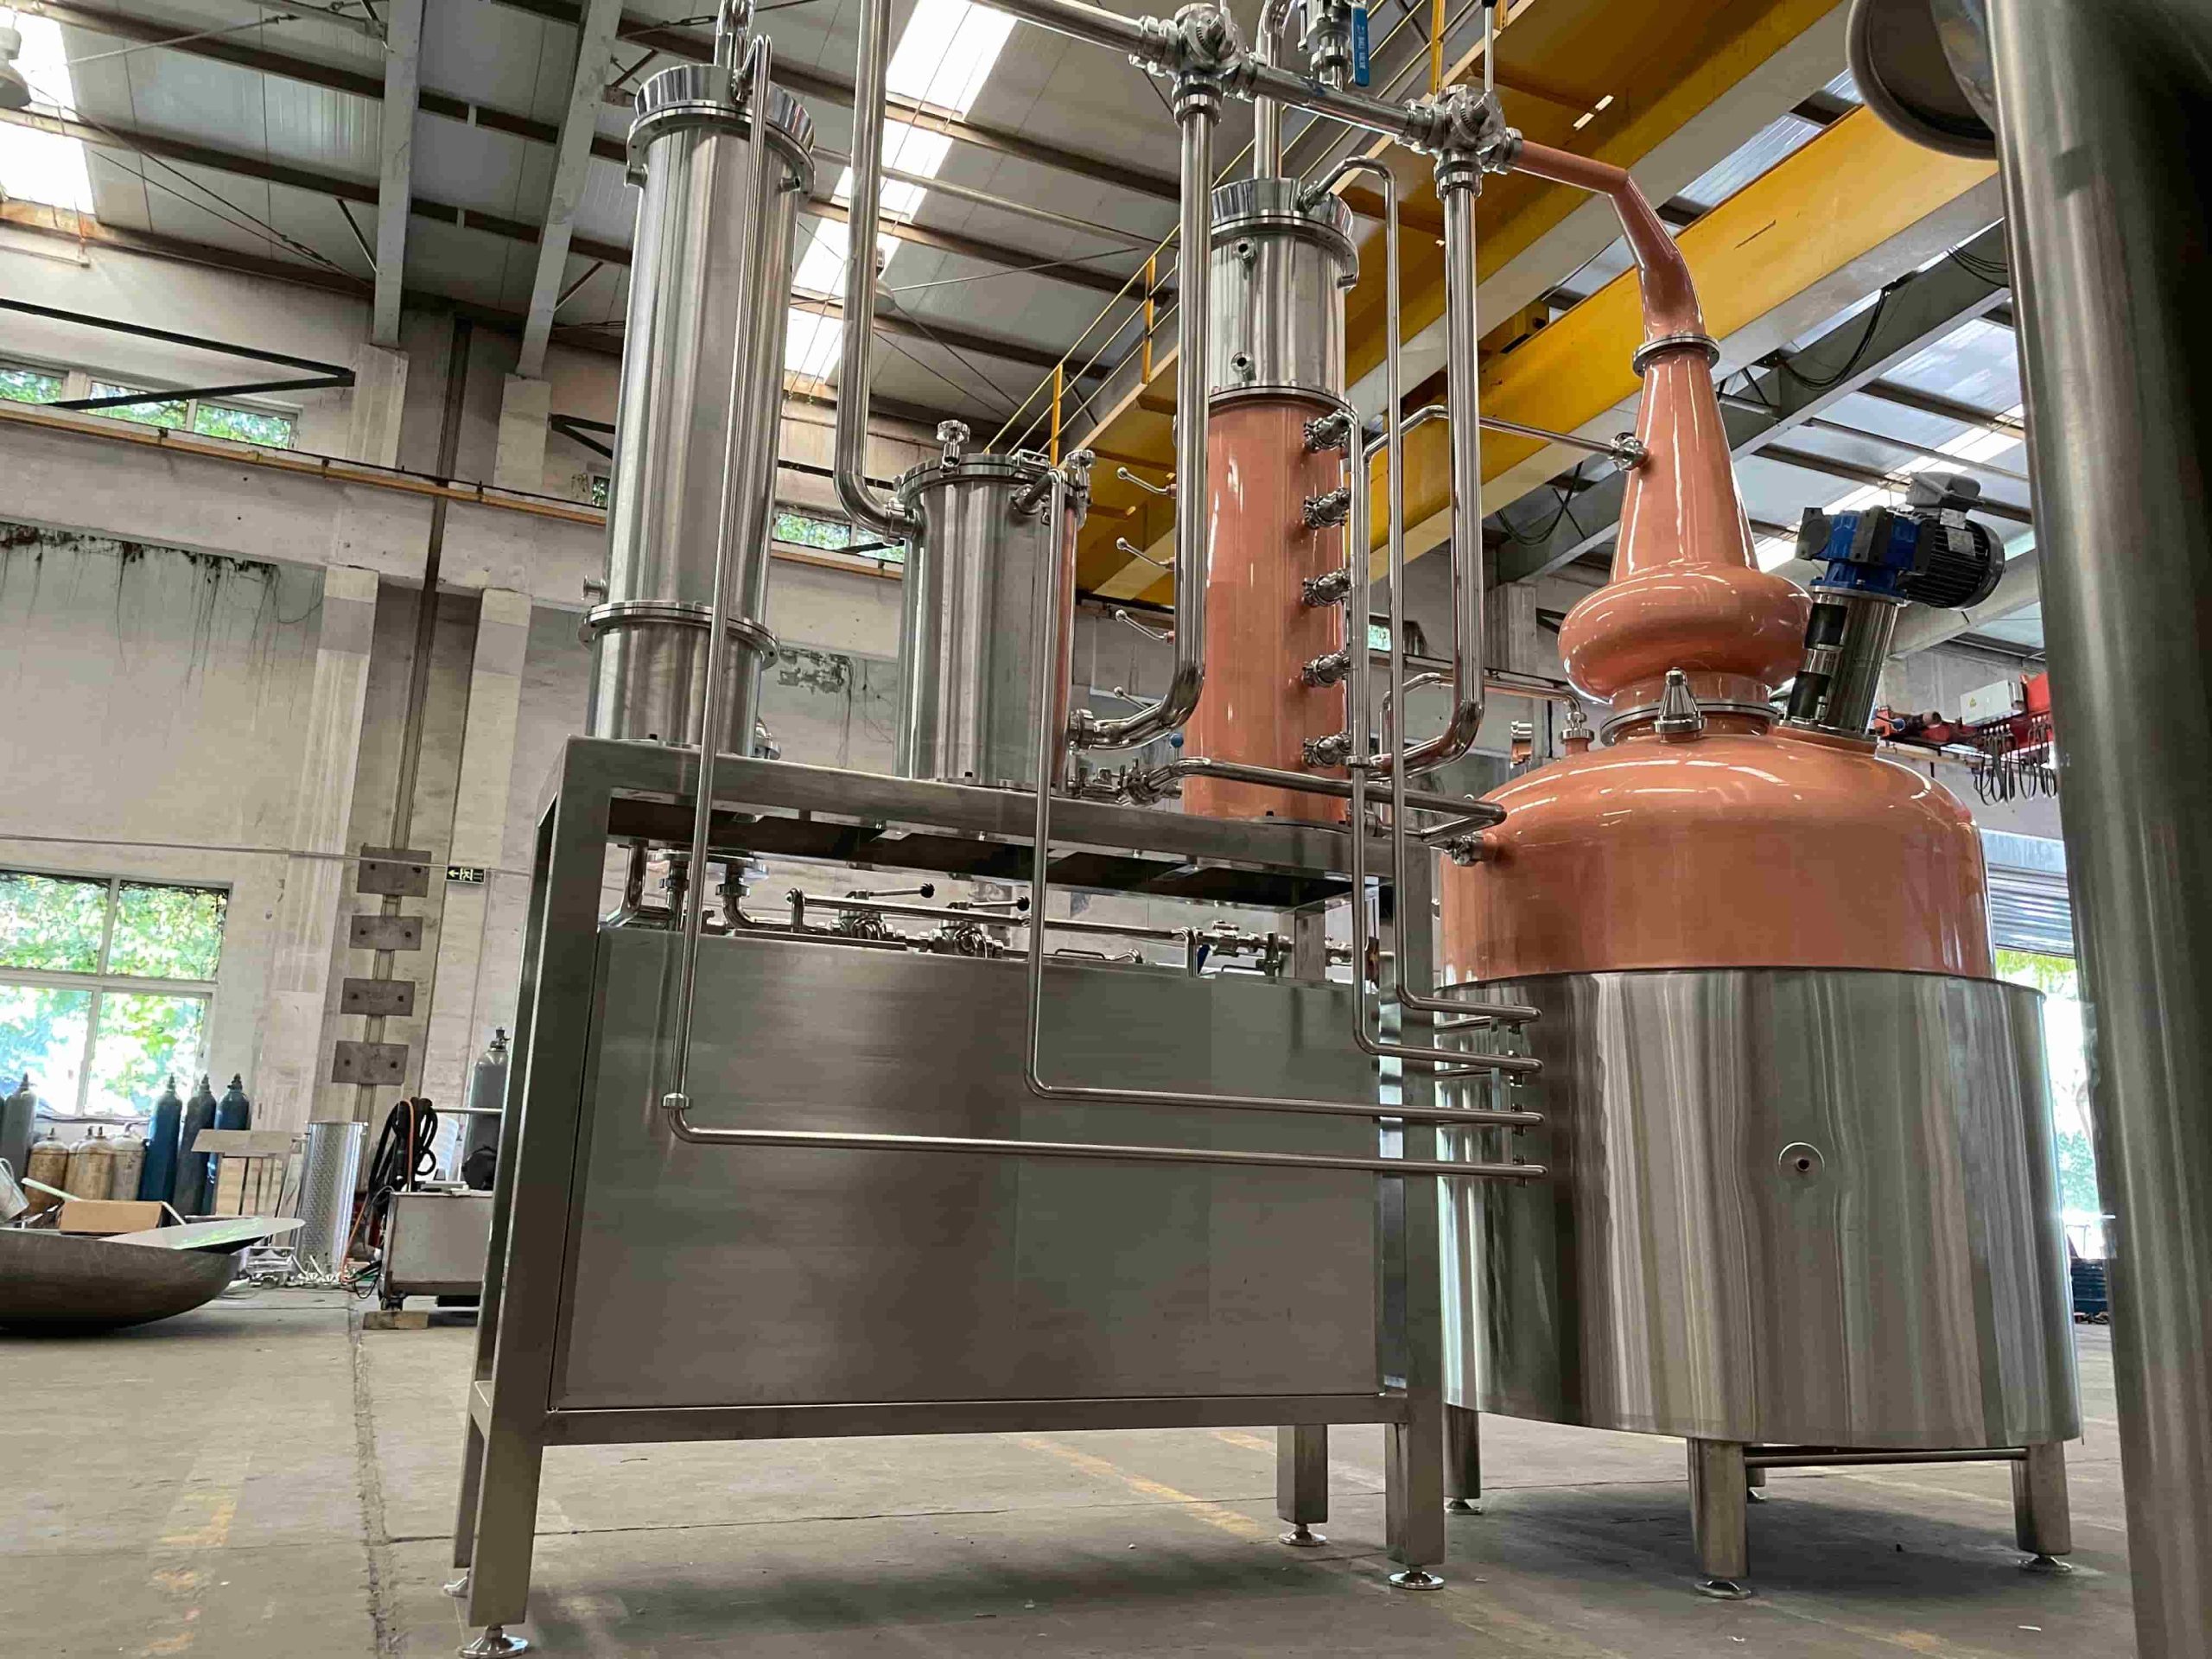
SKE’s pot stills have inner copper materials with stainless steel cladding. They include explosion-proof motors, agitators, glass manways, spray balls, temperature gauges, safety valves, and pressure gauges. You can choose steam or electric heating based on your facility.
Column Still
A column still is designed for more efficient separation. It can be used for continuous or semi-continuous production. Column stills are widely used for vodka and neutral spirits. These need a cleaner, more concentrated product.
SKE’s column stills use bubble caps inside the column. Each plate has red copper bubble caps, sight glasses, CIP balls, and discharge valves. The number of plates determines the final alcohol content.
Comparison Table
| Feature | Stainless Steel Pot Still | Column Still |
|---|---|---|
| Operation | Batch | Continuous or semi-continuous |
| Common Uses | Whiskey, rum, brandy | Vodka, neutral spirits |
| Spirit Character | Richer, more complex | Cleaner, more neutral |
| Production Efficiency | Moderate | High |
| Best For | Flavor-focused spirits | High-volume, high-purity production |
For some projects, SKE offers hybrid systems. These combine a pot still with a rectification column. This gives distillers more control over alcohol concentration and flavor.
Why Industrial Steam Distillation Equipment Matters
For medium and large-scale production, industrial steam distillation equipment has clear advantages. Steam transfers heat evenly through a jacket or heat exchanger. This reduces hot spots and makes temperature control easier.
Key parts of a steam system include:
-
Steam jackets
-
Steam control valves
-
Temperature sensors
-
Pressure monitoring
-
Condensate recovery
-
Heat exchangers
-
Automated process control
Steam heating is energy-efficient. It can work with a central boiler system. This is especially useful when a distillery already has steam utilities from brewing operations. SKE designs steam systems based on your production capacity and process needs.

Complete Distillation System Components
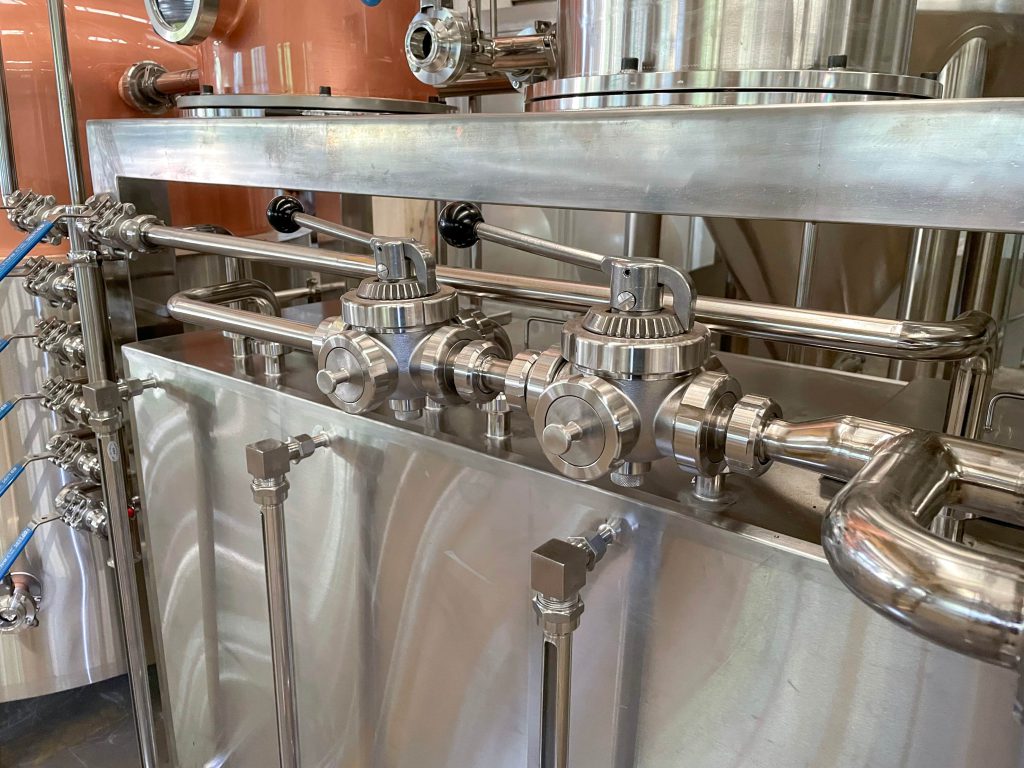
A complete distillation system includes several connected parts. Each part has a specific job.
| Component | Function | Design Consideration |
|---|---|---|
| Pot Still | Holds and heats fermented wash | Capacity, heating method, material |
| Distillation Column | Improves alcohol separation | Height, plates, internal design |
| Dephlegmator | Controls reflux and condensation | Temperature and vapor control |
| Gin Basket | Holds botanicals for vapor infusion | Size and loading method |
| Condenser | Converts vapor into liquid | Heat-transfer capacity |
| Control System | Monitors and controls the process | PLC, HMI, sensors, valves |
Dephlegmator
The dephlegmator is a tube-type heat exchanger at the top of the distillation column. It partially condenses vapor and sends distillate back to the pot. The cooling water inlet usually has a pneumatic or manual PID valve for temperature control.
Gin Basket
The gin basket lets you use botanicals in the vapor path. Hot vapor enters from above, passes through the botanicals, and exits at the top. This creates a clean, high-quality product.
Condenser
The condenser turns vapor into liquid. Like the dephlegmator, it has a cooling water inlet and outlet with temperature control.
Spirit Parrot
The spirit parrot connects between the condenser and spirit storage tanks. It holds an alcoholmeter so you can see real-time alcohol percentage readings during distillation.
Energy Efficiency and Cost Savings
Energy use is a major operating cost for commercial distilleries. A well-designed system can save you money on utilities.
Ways to save energy include:
-
Efficient steam heating
-
Good insulation
-
Optimized condenser design
-
Condensate recovery
-
Heat recovery systems
-
Improved process control
-
Efficient column operation
Heat exchangers can recover useful heat from hot process streams. This heat can be used for other production needs. Energy efficiency should be considered during the engineering stage, not added later.
Safety and Compliance
Safety is essential in any distillery. Alcohol vapor is flammable. Equipment and electrical systems must meet safety requirements and hazardous-area classification.
A professional system includes:
-
Pressure relief devices
-
Temperature and pressure monitoring
-
Emergency shut-off systems
-
Proper ventilation
-
Safe steam controls
-
EX-rated electrical components
-
PLC-based process control
SKE works with customers to define technical requirements before manufacturing. This ensures equipment matches the intended application and local regulations.
Why Choose SKE for Your Distillery Equipment?
Engineering Experience
SKE has decades of experience designing and manufacturing brewing and beverage equipment. This expertise applies directly to projects that combine fermentation, distillation, storage, and packaging.
Customized Design
SKE does not use a one-size-fits-all approach. Equipment is designed according to capacity, spirit type, building layout, heating method, and automation needs.
Complete System Integration
A distillery needs more than a still. SKE provides complete solutions including:
-
Brewing equipment
-
Distilling equipment
-
Fermentation tanks
-
Package and filling systems
-
CIP cleaning systems
-
Process technology support
Quality Materials
Food-grade stainless steel is used for process-contact parts. Material selection can be adjusted to meet project requirements.
Project Support
From early discussion and equipment design to manufacturing and installation guidance, SKE supports customers through all project stages. We offer a one-year warranty and whole-life engineering support.
Frequently Asked Questions
Q1: What is industrial distillation equipment?
Industrial distillation equipment is used to separate and concentrate alcohol from fermented liquids on a commercial scale. A complete system may include stills, columns, condensers, dephlegmators, heating systems, pumps, valves, and control systems.
Q2: What is the difference between a pot still and a column still?
A pot still works in batches and is often used for whiskey and rum where flavor is important. A column still provides more efficient separation and is widely used for high-volume production and neutral spirits like vodka.
Q3: Is steam heating suitable for large distilleries?
Yes. Steam heating is widely used in large-scale distillation because it provides controlled and even heat transfer. It can also connect to a central boiler and other plant utilities.
Q4: What material is best for an industrial still?
Food-grade stainless steel is a common choice because it provides strength, durability, and easy cleaning. Copper parts may also be used where they help the distillation process and spirit character.
Q5: Can SKE design a complete distillation system?
Yes. SKE provides customized distillation systems based on spirit type, production capacity, heating method, facility layout, and automation requirements.
Q6: Can SKE equipment be used for whiskey, vodka, gin, and rum?
Yes. Equipment configuration can be adapted for different spirits. Pot stills are commonly used for whiskey and rum. Column systems are often used for vodka and neutral spirits. Gin production needs extra botanical infusion equipment like the gin basket.
Conclusion
For a production brewery entering the spirits market, choosing the right industrial distillation equipment is a critical investment. The equipment must provide stable heating, good separation, reliable condensation, safe operation, and consistent production.
Stainless steel pot stills, column stills, industrial steam distillation equipment, condensers, and automated controls each play an important role. The best solution depends on your spirit, production capacity, process requirements, and future growth plans.
SKE provides customized industrial distillation equipment and complete distillery solutions for commercial and large-scale production. From individual stills to integrated systems, our engineering team can help develop equipment that fits your production goals.
If you are planning a new distillery or expanding an existing production line, SKE can help you evaluate the right equipment configuration for your project.
- Facebook: SKE Equipment Facebook
- Email: info@skeequipment.com
Fill out the contact form below for customized solutions. We fully support all your production equipment demands for breweries and beverage plants.